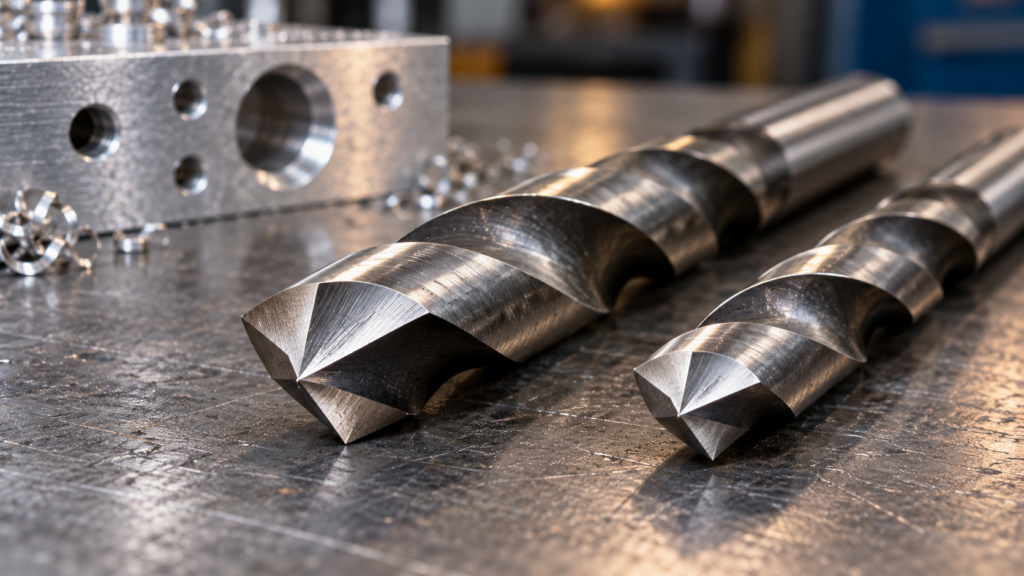
The drill point length formula is h = D ÷ [2 × tan(θ ÷ 2)], where D is drill diameter and θ is the included point angle. For an ideal conical point, a 118° drill has a point length of about 0.3004 × D; a 135° drill has about 0.2071 × D.
This extra length matters when a drawing requires a full-diameter blind hole. The drill tip must travel beyond the usable cylindrical depth. Here is how to calculate that allowance without confusing tip depth with full-diameter depth.
Drill point length formula and angle convention
Imagine a section through the drill axis. Half the cone forms a right triangle: the opposite side is D/2, the adjacent side is point length h, and the angle at the tip is θ/2. Therefore tan(θ/2) = (D/2)/h. Rearranging gives:
h = (D/2) ÷ tan(θ/2)
Use degrees when entering the angle in a calculator. Keep diameter and point length in the same length unit. The included angle is the full angle across the point, not the half-angle used inside the tangent calculation.
This is an ideal cone model. Split points, web thinning, special tip profiles and regrinds may differ. When the manufacturer supplies an actual point-length dimension, use that value for the specific tool.
118° vs 135° drill point length
The Haas machinist’s reference guide lists rounded shop factors of 0.300 × diameter for 118° and 0.207 × diameter for 135°. The table below uses the trigonometric formula and rounds the calculated results.
| Drill diameter | 118° point length | 135° point length |
|---|---|---|
| 0.250 in | 0.0751 in | 0.0518 in |
| 0.500 in | 0.1502 in | 0.1036 in |
| 10 mm | 3.0043 mm | 2.0711 mm |
| 20 mm | 6.0086 mm | 4.1421 mm |
For the same diameter, the wider 135° included angle produces a shorter ideal point. That geometric difference alone does not tell you which drill suits a material. For example, Gühring’s drill catalogue includes different tool families with 118° and 135° points. Choose the complete drill design, grade and coating for the workpiece.
Blind-hole depth: add the point allowance
If the drawing specifies full-diameter depth L, the ideal tip depth from the same surface is:
Tip depth = full-diameter depth + point length = L + h
For a 0.500 in drill with a 118° point and a required 1.000 in full-diameter depth, h = 0.1502 in. The calculated tip depth is 1.1502 in. If surface Z is zero and drilling moves in negative Z, that corresponds to a nominal endpoint near Z −1.1502.
This is a geometry example, not a ready-to-run program. Confirm the drawing’s depth convention, tool-length reference, remaining wall and machine setup before using an endpoint. If the specified depth is already measured to the drill tip, do not add the allowance a second time.
Metric example: a 10 mm drill
Suppose a 10 mm drill has a 135° included angle and the part needs 18 mm of full-diameter depth. Calculate h = 5 ÷ tan(67.5°) = 2.0711 mm. Then add 18 + 2.0711 = 20.0711 mm nominal tip depth.
Changing to a 118° drill changes the ideal allowance to 3.0043 mm. The nominal tip depth becomes 21.0043 mm. Recheck the allowance whenever the tool or point grind changes.
Through holes and tapped holes need separate checks
For an ideal through hole, the full-diameter portion must reach the exit surface. Stock thickness plus point length is the geometric starting point for tip travel. Any additional breakthrough distance must suit the tool, burr requirements, backing arrangement and clearance behind the part; there is no universal extra value.
A tapped blind hole adds another requirement. Drill-point space is not usable full-diameter hole depth, and drilled depth is not the same as full thread depth. Account for the tap’s lead and required clearance using the tap maker’s drawing.
Check your result with the free calculator
Use the drill point calculator to enter diameter and included point angle. For cutting parameters, open the drilling speed and feed calculator. Use its material guidance as a starting point and check the actual toolmaker’s data.
Before releasing the job, record the point angle, diameter, requested depth convention and calculated allowance together. Use the inch-to-millimetre converter when dimensions arrive in a different unit system.
Common questions
Is drill point length the same as flute length?
No. Point length is the axial distance occupied by the tip geometry. Flute length describes a different part of the drill and must be checked separately for reach and chip evacuation.
Can I use diameter × 0.3 for every drill?
No. That is a rounded shortcut for a 118° ideal point. A 135° point uses approximately 0.2071 × diameter, and special drill tips may need the manufacturer’s actual dimensions.
Does the formula work in inches and millimetres?
Yes. Enter the diameter in your chosen unit; the result is in that same unit. Angle remains in degrees.
Put the formulas to work
Use our free calculators for speeds, feeds, angles, hole patterns and dimensional checks. For content corrections, contact CNC TrueCut.
Tooling and insert brands: discuss an advertising partnership.