Milling & geometry
Calculate spindle speed, chip load, angles and hole patterns.
TOOLS FOR THE SHOP FLOOR
Free CNC calculators, clear formulas, and practical tooling guides. Find your numbers. Understand your next cut.
in / mm · Formulas included · Free to use
PRECISION STARTS WITH THE NUMBERS
START WITH YOUR OPERATION
Calculate spindle speed, chip load, angles and hole patterns.
Work out RPM, feed and taper Z length in inches or millimetres.
Choose twist, spade or U-drill calculations, with material guidance.
TOOLING, EXPLAINED
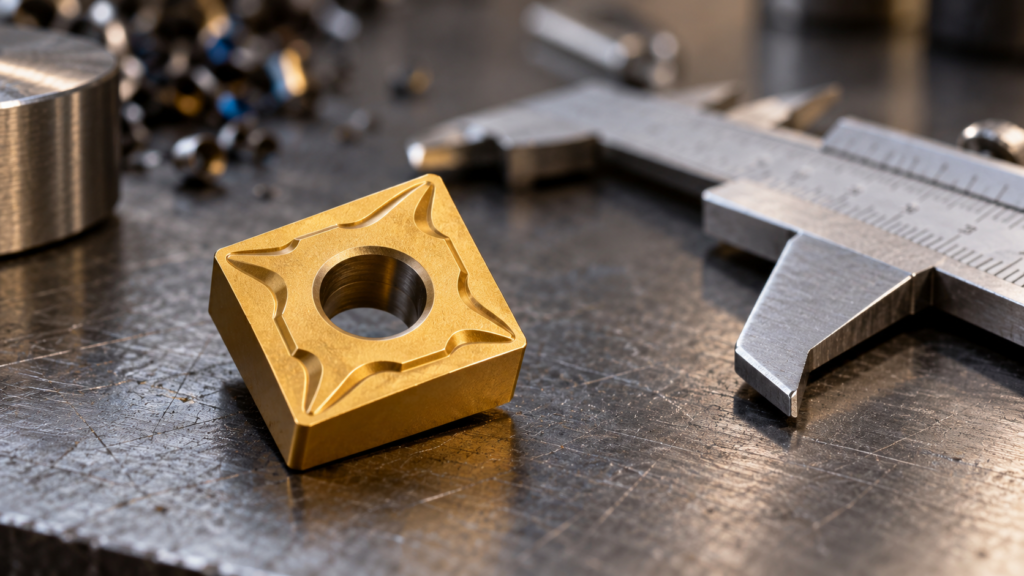
CNMG, DNMG or VNMG? Compare shape and profile access, then check the material, grade, chipbreaker and holder.
CNMG · 80°
DNMG · 55°
VNMG · 35°
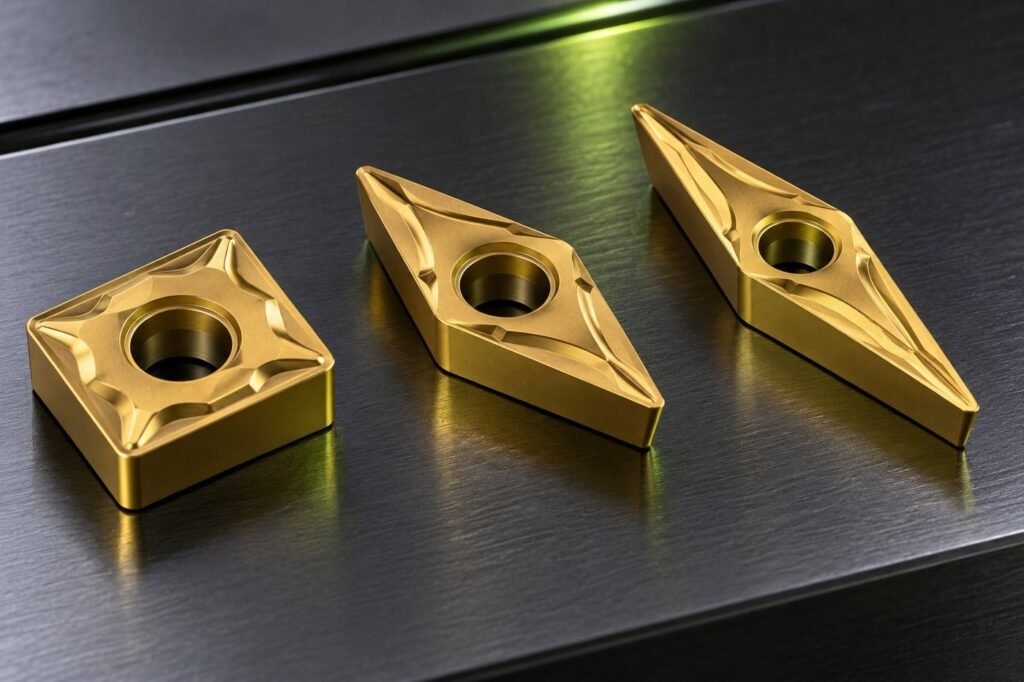
Tooling illustration. Confirm the exact insert and holder specifications.
KEEP THE MATH HANDY
Open the free workbench for milling, drilling, turning, tapping, threading and X-to-Z taper geometry.
FREE MACHINIST TOOLS
Milling, drilling, lathe, tapping and threading calculations in Imperial and Metric units.
| THREAD VALUE | COMPUTED RESULT |
|---|---|
| Selected standard | |
| Pitch | |
| Lead | |
| Included angle / form | |
| Theoretical sharp-V height | |
| Basic external minor diameter | |
| Basic internal minor diameter | |
| Taper / specification note |
Educational starting point only. Verify against the cutting-tool manufacturer’s data, machine limits and a safe prove-out. Thread diameters are basic 60° geometry and do not include class or tolerance.
Build a reviewable starting program. Confirm your exact control format and every value before running.
Mandatory verification: Fanuc G76 address meanings and integer scaling vary by control generation and machine builder. Confirm diameter/radius conventions, P/Q scaling, taper sign, tool orientation, clearance, spindle direction, insert data and the machine manual. Never run generated code without simulation, single-block and a safe prove-out.
Find angles, missing sides and taper geometry. All angles are measured in degrees.
Right triangle: θ = atan(rise / run); travel = √(run² + rise²). With angle and run: rise = run × tan(θ); travel = run / cos(θ). The other acute angle is 90° − θ.
Find Z: Z = (major X − minor X) / (2 × tan θ). θ is the angle to the spindle axis. For a full included angle A, use θ = A / 2. Example: X2 to X1 at 30° to the axis gives Z = 0.866025 in. At a 30° included angle, Z = 1.866025 in.
Taper: radial change = (D − d) / 2; half-angle θ = atan((D − d) / (2L)); included angle = 2θ; diameter taper per unit length = (D − d) / L. Enter the axial length, not the sloping surface length. Values use one common length unit.
The diagram illustrates the angle convention and is not to scale. Confirm whether your drawing or machine setup specifies the half-angle or included angle.
LEARN THE WHY BEHIND THE NUMBERS
FOR TOOLING BRANDS
Reach CNC TrueCut visitors with relevant insert, tooling and machining partnerships.